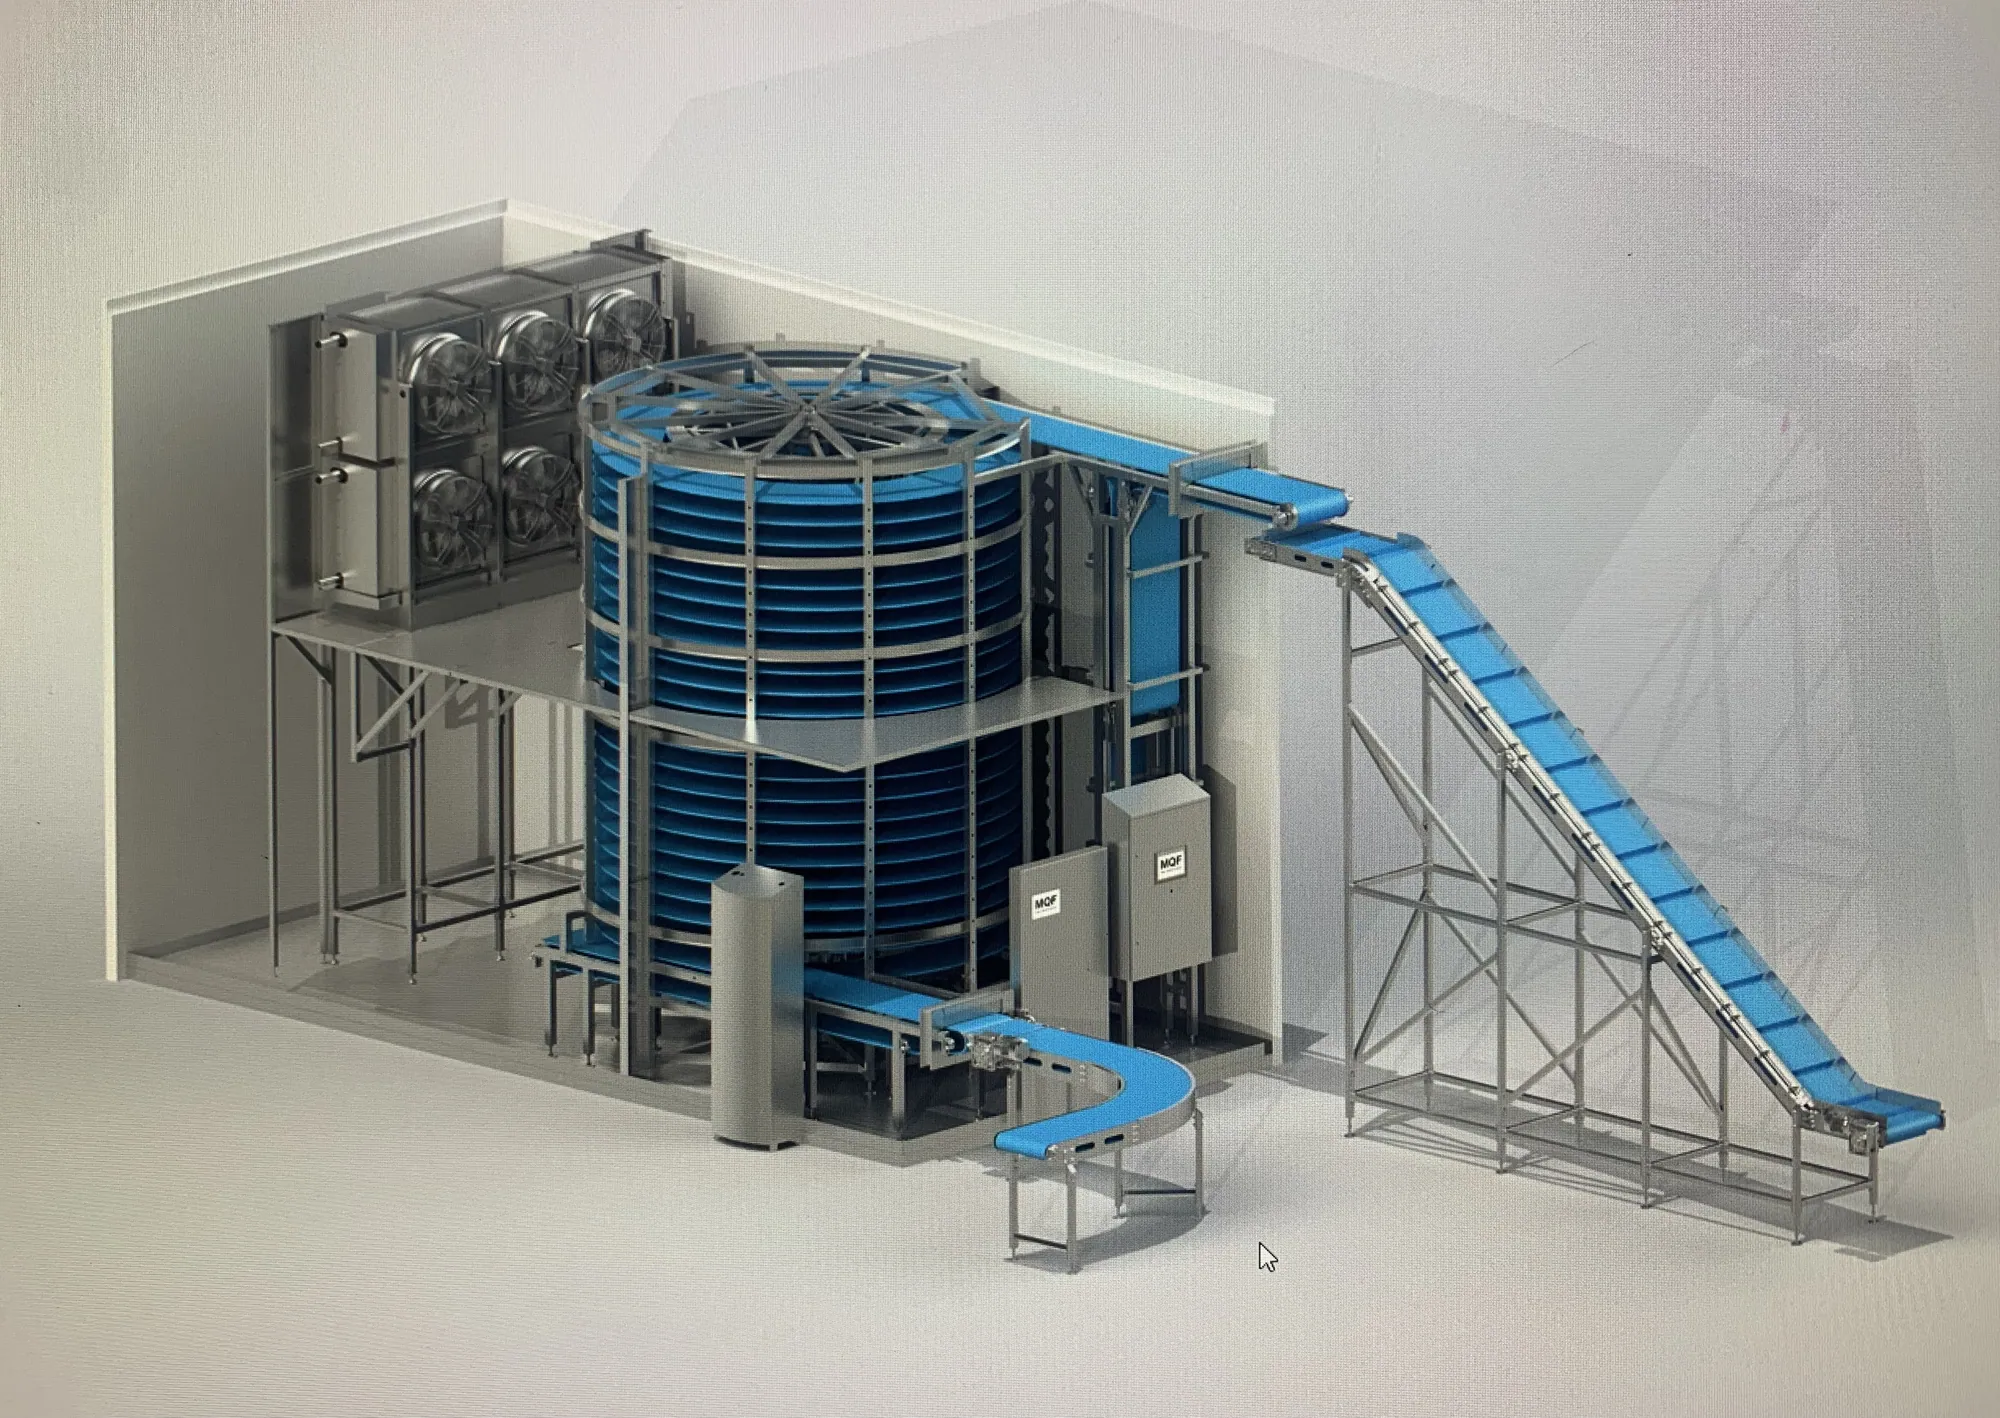
Hygienic Conveyors
Clean, contamination-free handling for food, pharma, cosmetics and chemicals.
Hygienic conveyors are specially engineered systems that move products safely, cleanly and without contamination — particularly in food, pharmaceutical, cosmetic and chemical industries. Unlike standard conveyors, they are built to strict sanitary material and design criteria.
System types for every need.
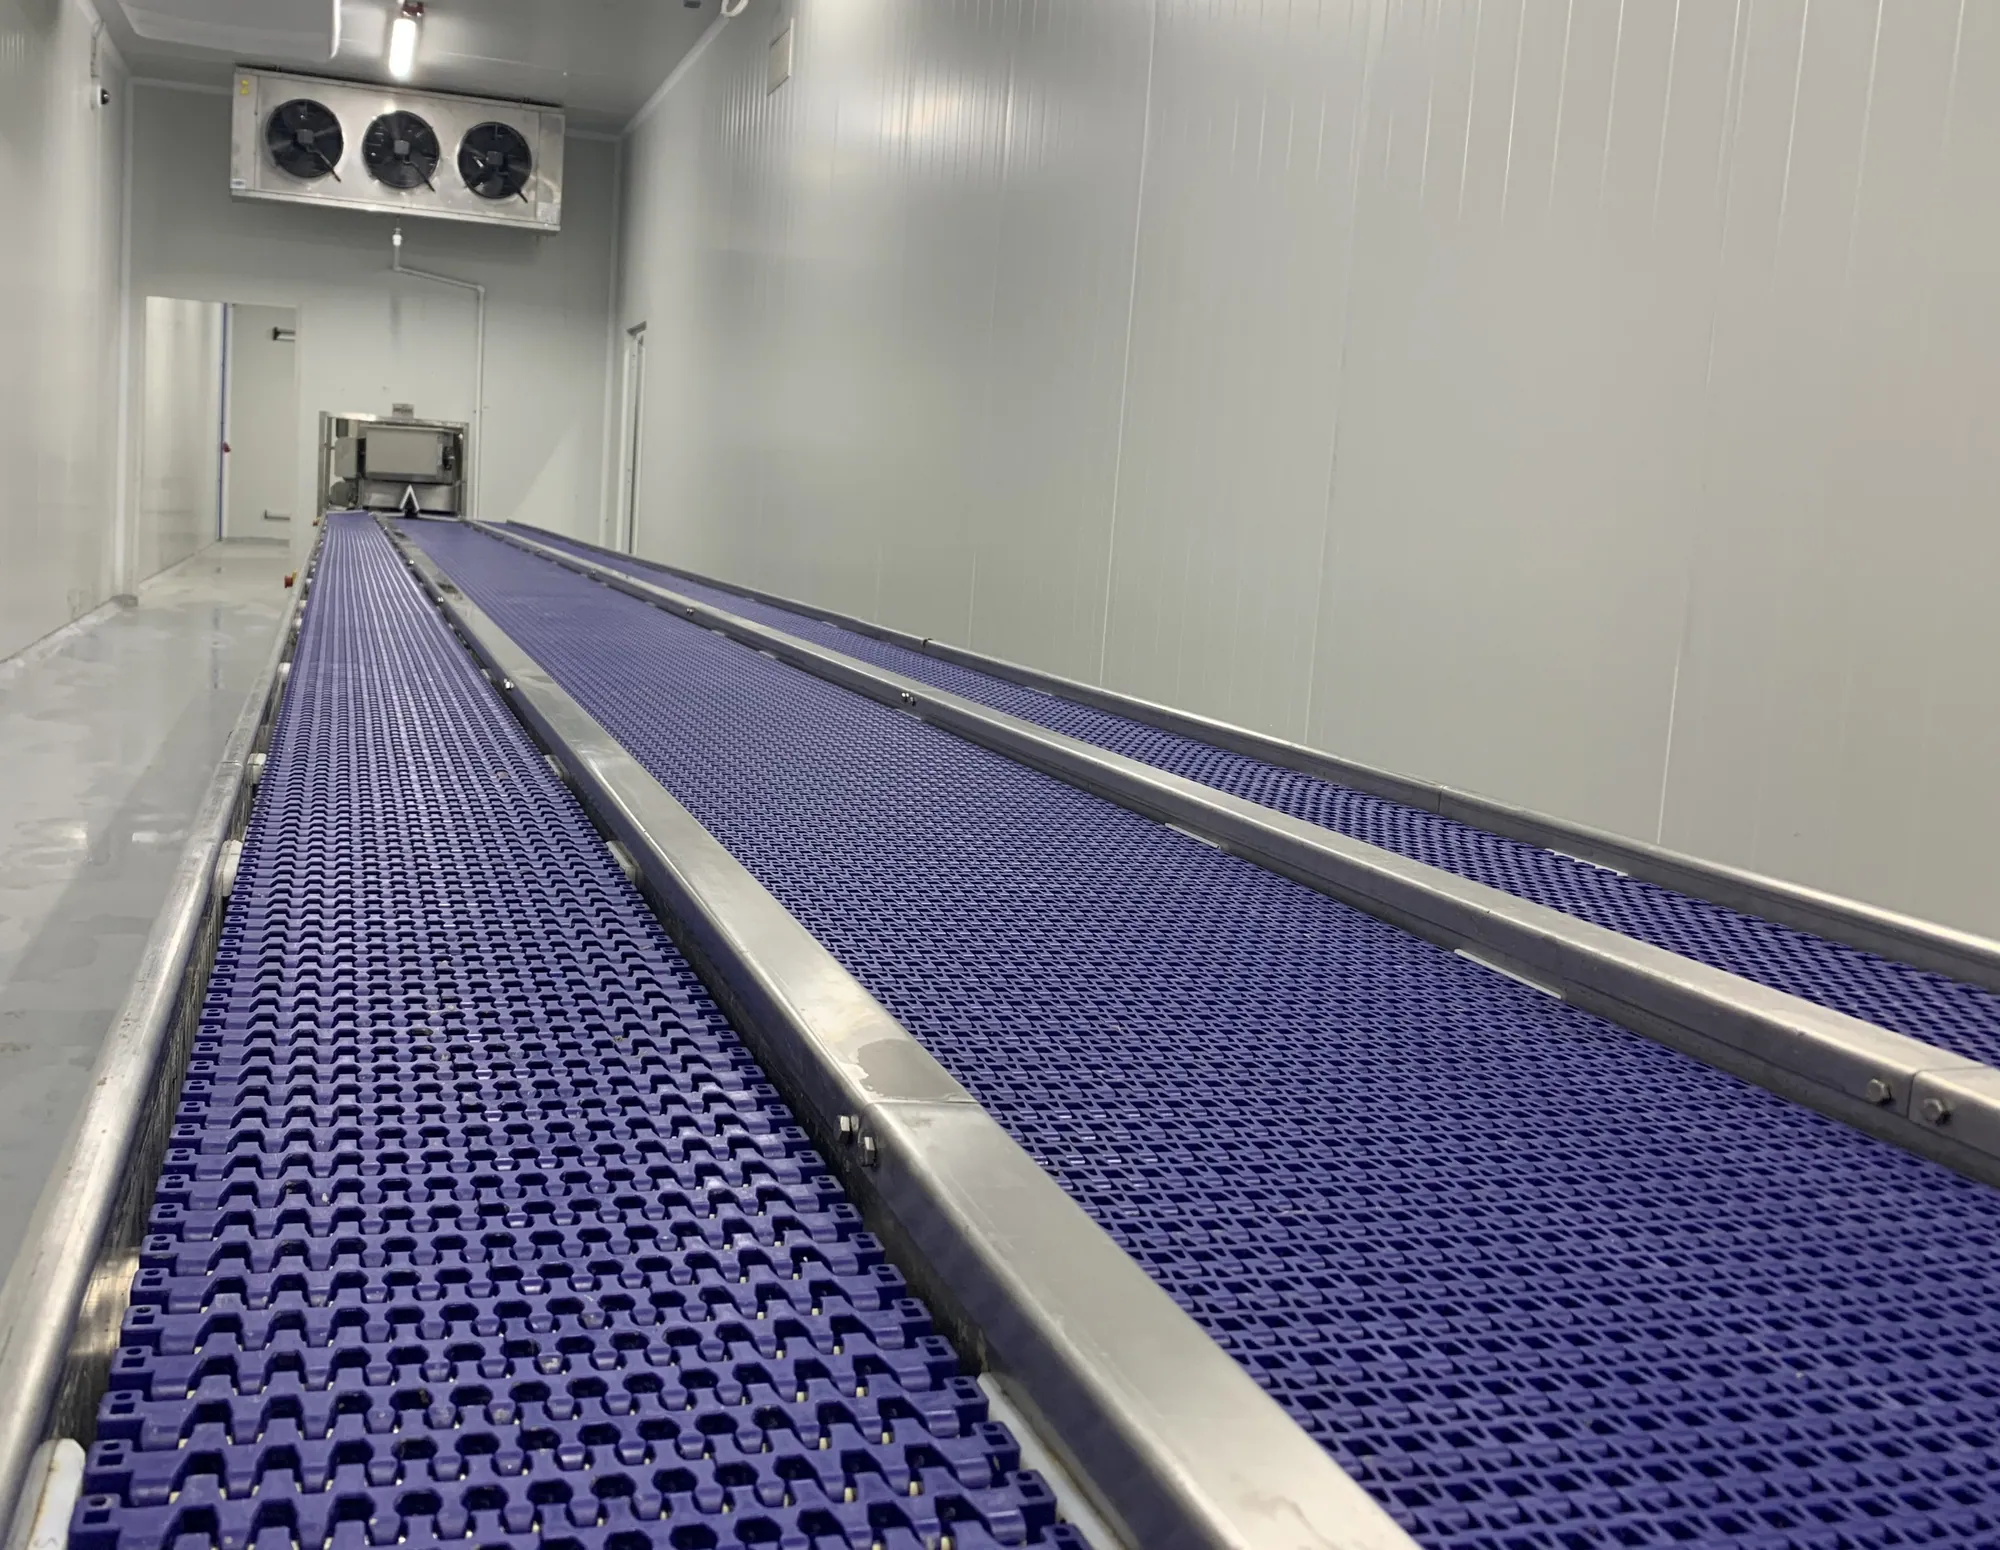
Straight Conveyors
These systems are engineered for the safe and secure transport of products along a linear path, specifically designed for industries demanding stringent hygiene and sanitation standards, such as food, pharmaceuticals, and chemicals.
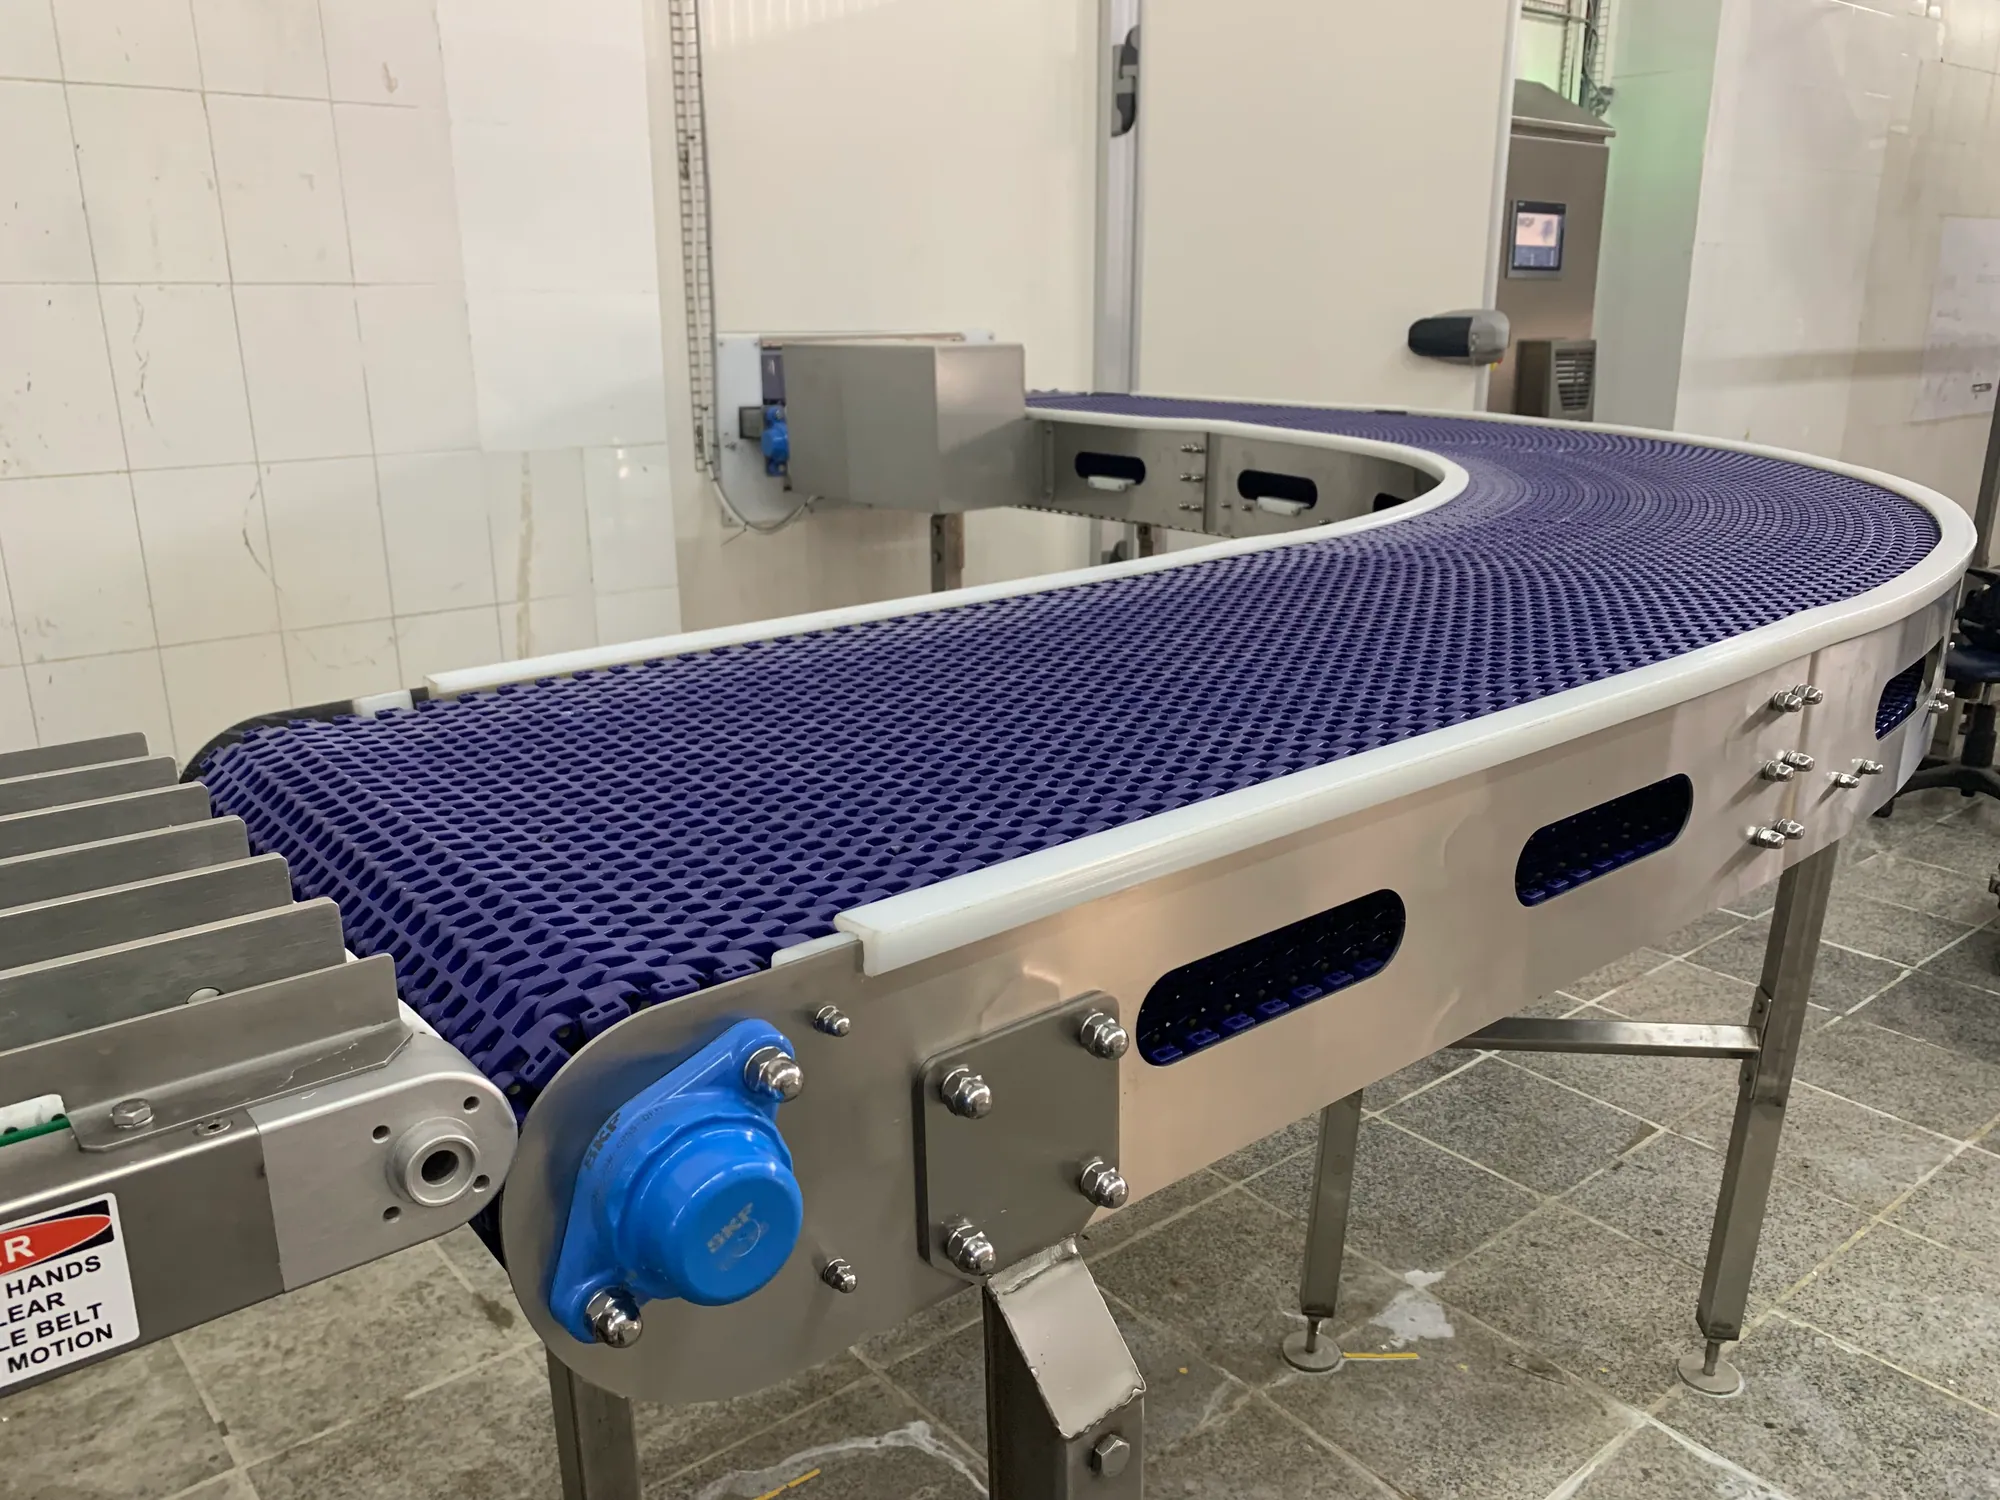
Curved Conveyors
These conveyors are utilized to change product direction within production lines, maximize facility floor space efficiency, or provide seamless transitions between lines at varying heights. Turning angles can be custom-manufactured to match specific layout and operational requirements.
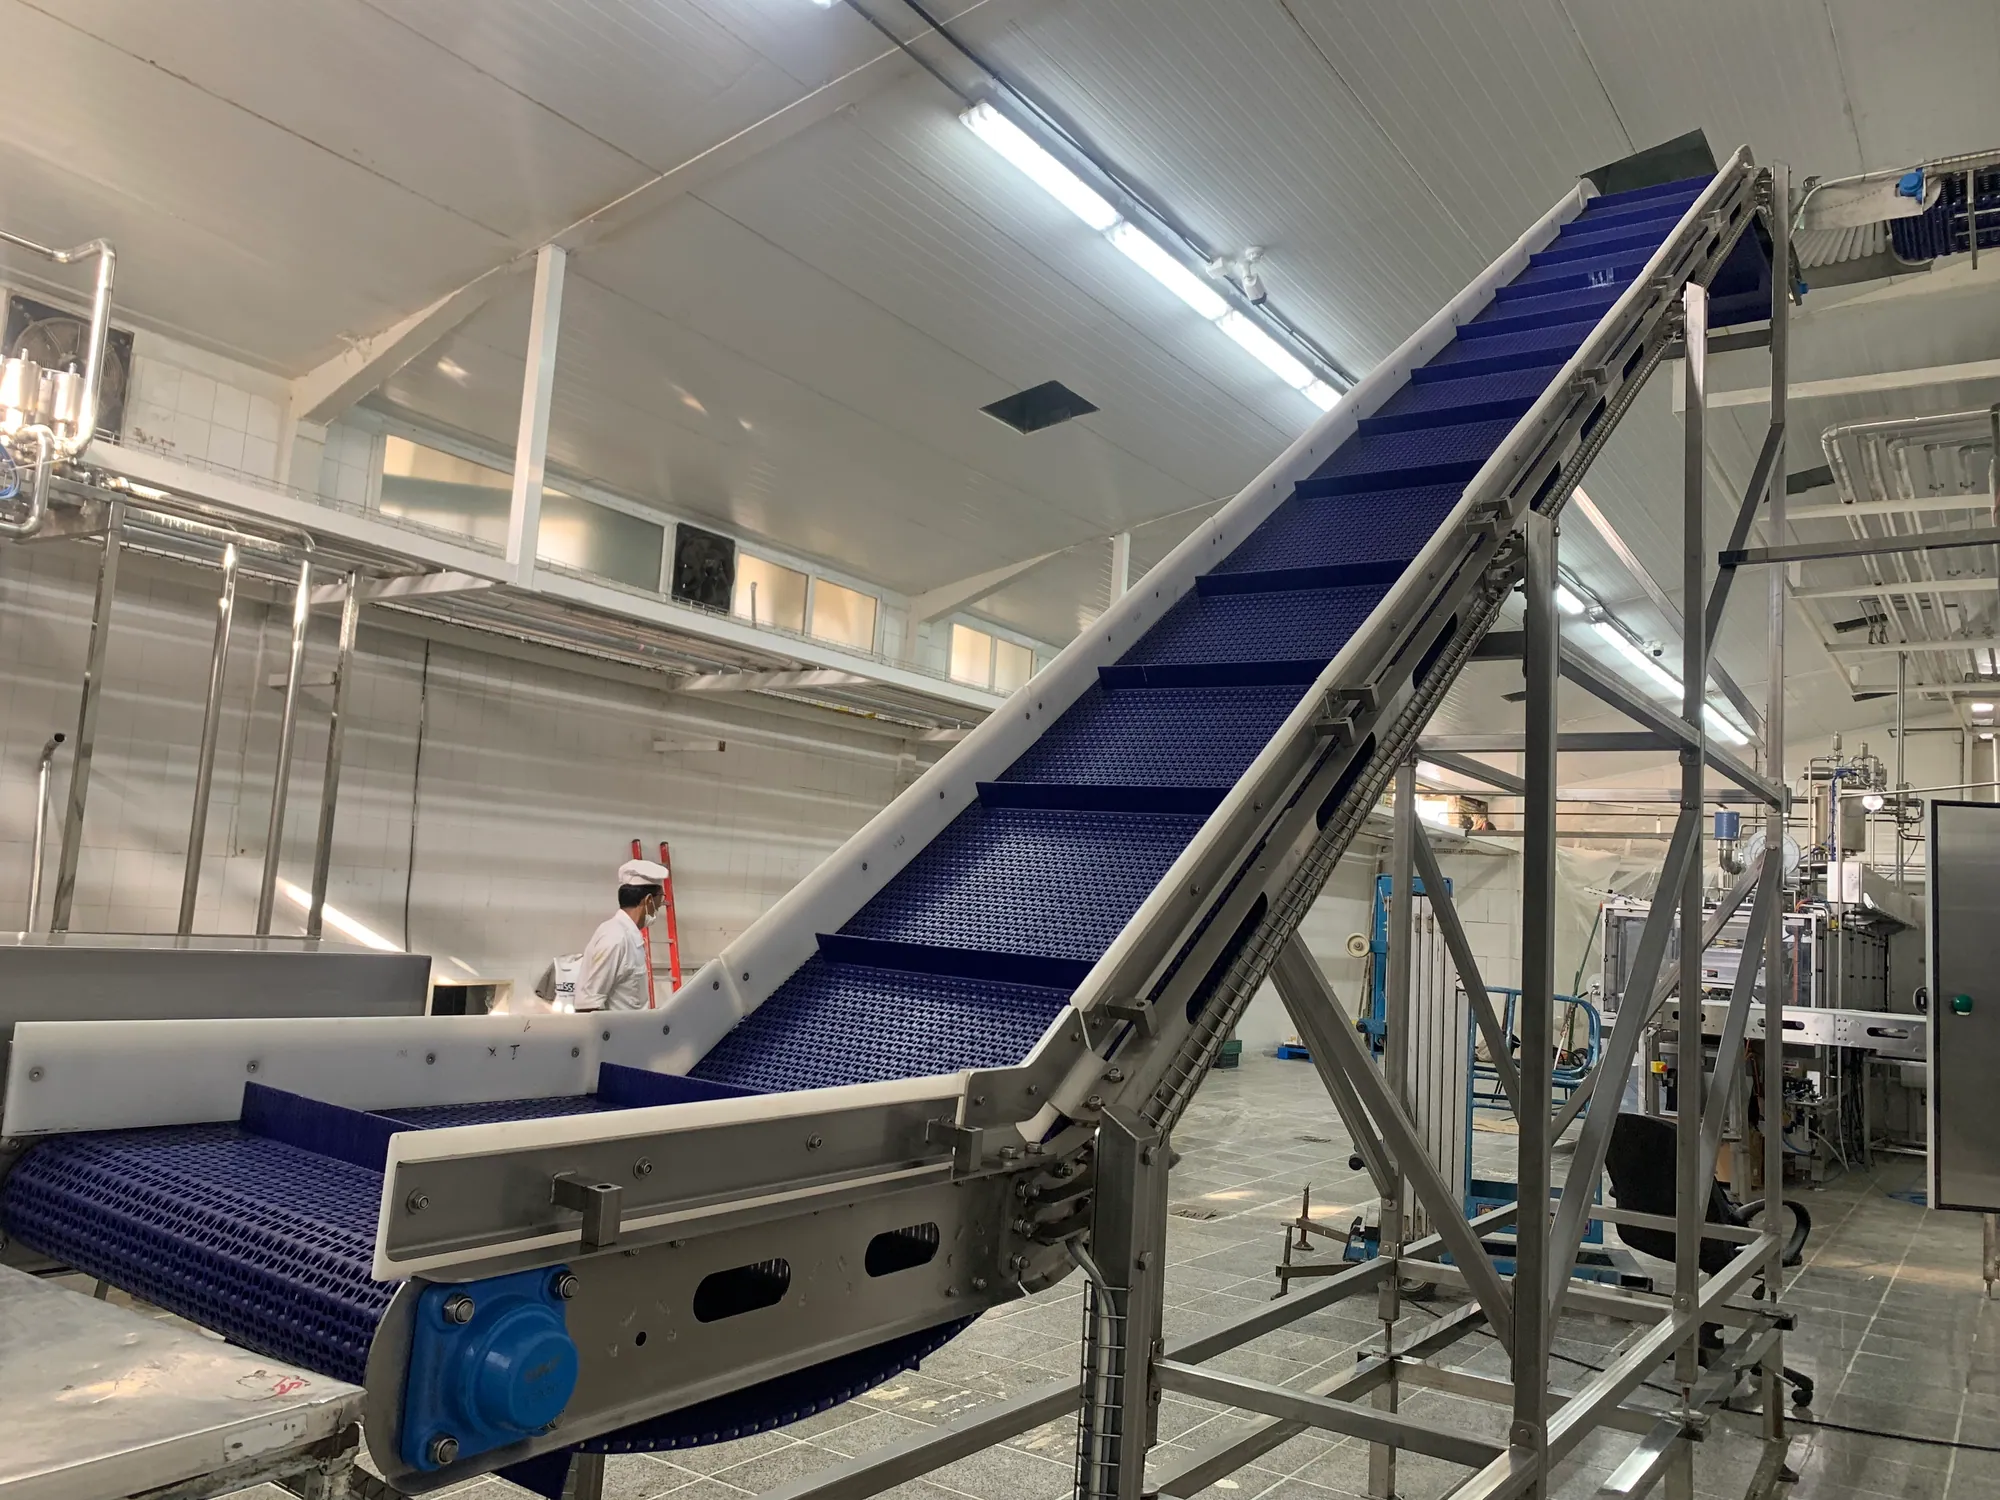
Z-Type Conveyors
These conveyors are designed for vertical product transport between different elevations, effectively elevating or lowering products to specific heights. Due to their unique engineering and structural design, they ensure smooth product handling without causing any damage or degradation.
Debris-Removal Conveyors (Integrated Scrape)
These specialized conveyors are engineered for the efficient transport and safe discharge of organic processing waste, including dough residues, fruit and vegetable peels, bone fragments, and rejected/defective packaged products across the food industry.
Conveying Food to the Future
Let's design the solution that suits your capacity.
We’ll create a design tailored to your product, capacity and process. Fill in the form and our team will get back to you shortly.